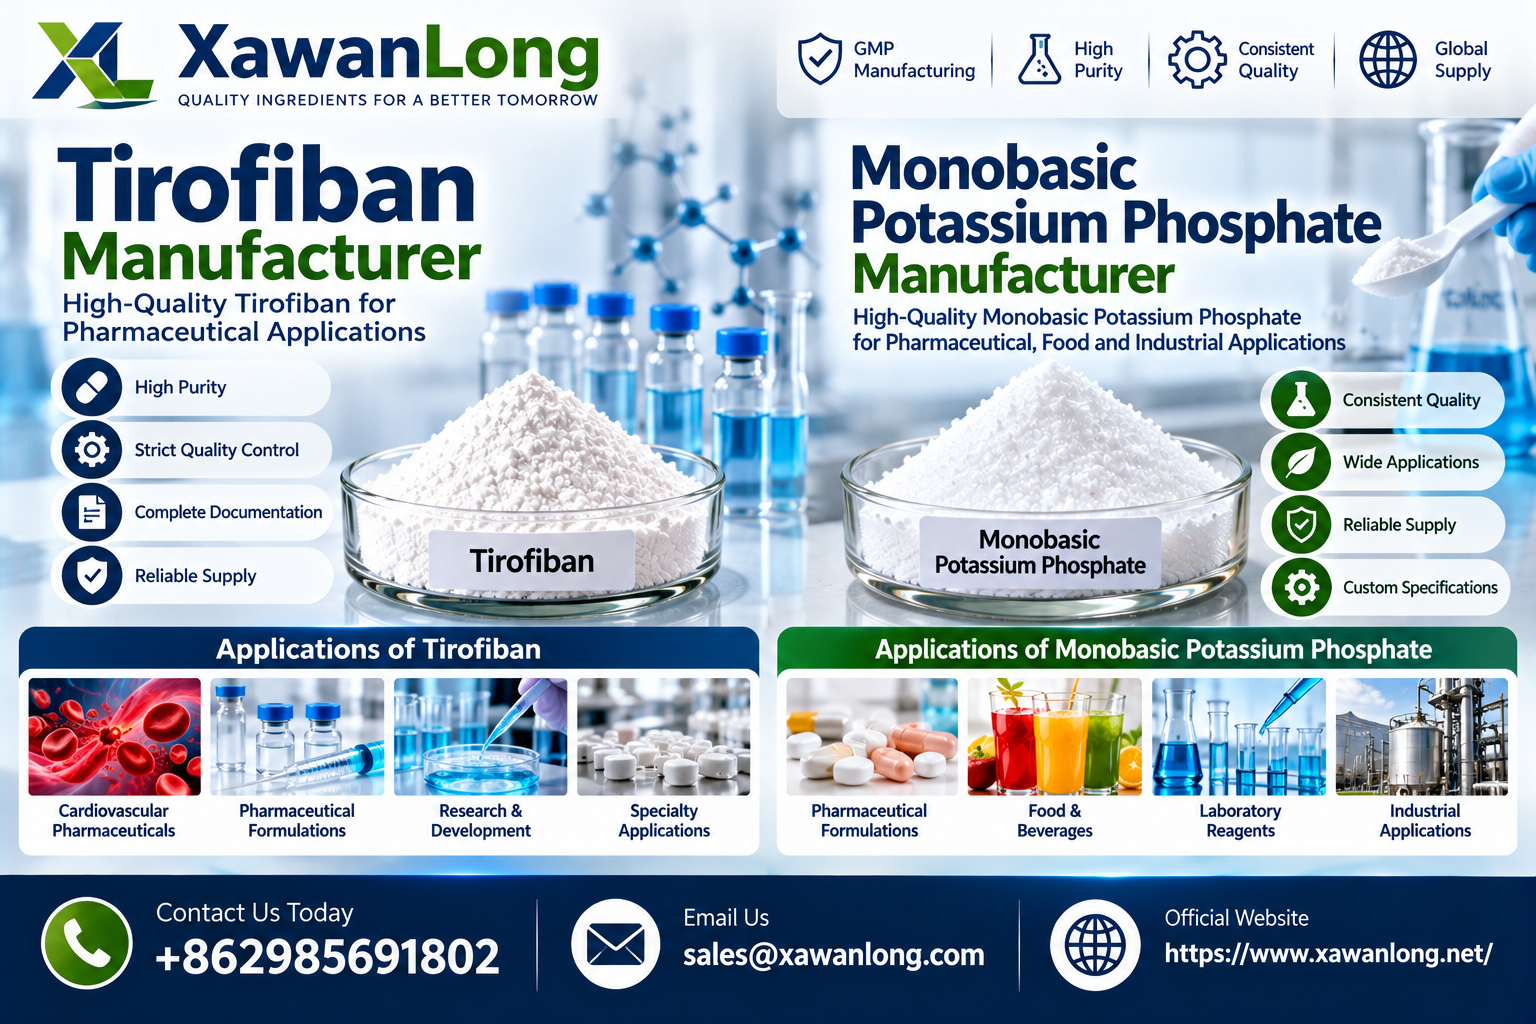
Global pharmaceutical sourcing is becoming more structured as manufacturers focus on raw-material consistency, technical documentation, traceability, and dependable supply. Within this changing environment, selecting an experienced Tirofiban manufacturer and a qualified Monobasic potassium phosphate manufacturer can help pharmaceutical companies strengthen procurement planning and reduce avoidable supply-chain risks.
Although tirofiban and monobasic potassium phosphate have very different roles, buyers assessing either material increasingly look beyond price. Manufacturing controls, analytical testing, documentation, packaging, storage, communication, and batch consistency can all influence supplier qualification.
Why Tirofiban Manufacturing Requires Careful Supplier Evaluation
Tirofiban is associated with pharmaceutical applications where product quality and manufacturing consistency require careful attention.
A professional Tirofiban manufacturer should operate through clearly defined procedures covering material handling, manufacturing, quality testing, packaging, and release.
Depending on the buyer’s intended application, important evaluation points may include:
- Product identity
- Assay requirements
- Related substances or impurities
- Manufacturing controls
- Batch traceability
- Analytical methods
- Packaging configuration
- Storage conditions
- Technical documentation
Customers should confirm that the specific material and supporting documentation are appropriate for their own regulatory market and intended pharmaceutical use.
Consistency Begins Before Final Testing
Quality cannot be created only through testing a finished batch.
Reliable pharmaceutical production begins with controlled raw materials and continues through every stage of manufacturing.
A qualified Tirofiban manufacturer may therefore establish procedures for:
Raw-Material Review
Incoming materials should be checked against predefined requirements before use.
Controlled Processing
Manufacturing steps should follow established operating procedures.
In-Process Monitoring
Relevant process parameters may need to be monitored throughout production.
Finished-Product Testing
The completed material should be assessed against the agreed specification before release.
Record Keeping
Production and quality records should provide appropriate traceability.
What Is Monobasic Potassium Phosphate?
Monobasic potassium phosphate, also called potassium dihydrogen phosphate, is commonly represented by the chemical formula KH₂PO₄.
Depending on its grade and specification, it may be used in pharmaceutical, laboratory, chemical, formulation, buffering, and other technical applications.
A dependable Monobasic potassium phosphate manufacturer should clearly identify the grade and quality specifications being supplied.
Important characteristics can include:
- Assay
- Identity
- Purity
- Physical appearance
- Moisture
- Relevant impurity limits
- Packaging
- Recommended storage
The correct grade should always be selected according to the intended application.
Why Product Grade Matters
Two materials with the same chemical name are not necessarily interchangeable.
Pharmaceutical, laboratory, and industrial grades may differ in:
- Purity requirements
- Analytical testing
- Impurity limits
- Manufacturing controls
- Documentation
- Packaging
- Intended use
This makes clear communication essential.
When contacting a Monobasic potassium phosphate manufacturer, buyers should specify the application and quality requirements rather than requesting only the chemical name.
The Role of Monobasic Potassium Phosphate in Formulations
Monobasic potassium phosphate may be selected in applications where phosphate chemistry or buffering is required.
Its suitability depends on the specific formulation, concentration, quality specification, and application requirements.
Consistent raw-material quality can help formulation teams achieve:
- More predictable processing
- Repeatable analytical results
- Better batch comparison
- Controlled formulation behavior
- More dependable manufacturing planning
For this reason, customers may evaluate both specification compliance and consistency across repeat orders.
Documentation Is Central to Pharmaceutical Sourcing
Technical documentation is increasingly important during supplier qualification.
Depending on the product and application, customers may request:
- Certificate of Analysis
- Product specification
- Safety Data Sheet
- Packaging information
- Storage recommendations
- Batch identification
- Quality questionnaires
- Regulatory-support documents where applicable
The required document package should be discussed before commercial supply begins.
Clear documentation can reduce delays during internal quality and regulatory reviews.
Why Certificates of Analysis Matter
A Certificate of Analysis provides test results for a particular production lot.
It allows customers to compare batch data against agreed specification limits.
For pharmaceutical ingredients, buyers should review the actual reported values rather than relying solely on a general statement that the material passed.
A strong quality relationship is based on transparent data and clearly understood specifications.
Traceability Helps Manage Quality Risk
Traceability allows manufacturers to connect a supplied lot with relevant production and testing records.
This becomes important if a customer needs to investigate:
- Analytical variation
- Specification concerns
- Packaging problems
- Transportation damage
- Customer complaints
Reliable traceability can make investigations faster and support stronger supply-chain oversight.
Both a Tirofiban manufacturer and a Monobasic potassium phosphate manufacturer should maintain batch identification appropriate to the supplied material.
Packaging Is Part of Material Protection
Packaging plays an important role after manufacturing is complete.
Suitable packaging helps protect pharmaceutical and chemical materials during storage and international transportation.
Customers should review:
- Container size
- Inner packaging
- Sealing method
- Product labeling
- Lot identification
- Storage instructions
Packaging requirements should ideally be confirmed before placing an order.
Storage Conditions Should Be Clearly Communicated
Manufacturers should provide appropriate storage guidance for supplied materials.
Customers, in turn, should ensure warehouse procedures are capable of maintaining the recommended conditions.
Important considerations may include:
- Temperature
- Moisture control
- Container closure
- Warehouse cleanliness
- Stock rotation
Correct storage helps preserve material quality after delivery.
Supply Continuity Is Increasingly Important
Pharmaceutical companies are giving greater attention to long-term supply reliability.
A product may meet technical requirements but still create operational difficulties if deliveries are unpredictable.
Procurement teams may therefore evaluate:
- Manufacturing capacity
- Typical lead times
- Repeat-order capability
- Commercial availability
- Packaging flexibility
- Export support
- Technical responsiveness
- Quality documentation
This broader approach can make supplier relationships more sustainable.
Technical Communication Reduces Delays
A complete purchasing enquiry can help suppliers provide more accurate technical and commercial information.
Customers should normally provide:
- Product name
- Required grade
- Specification
- Quantity
- Intended use
- Packaging requirements
- Destination
- Documentation expectations
Clear communication during the initial enquiry can prevent unsuitable material from progressing too far through the qualification process.
Frequently Asked Questions
What does a Tirofiban manufacturer do?
A Tirofiban manufacturer produces tirofiban-related pharmaceutical material according to defined manufacturing and quality requirements.
What should buyers review before purchasing tirofiban?
Buyers should evaluate specification, assay, impurities, documentation, packaging, storage requirements, and suitability for the intended market.
Is all tirofiban material suitable for pharmaceutical production?
No. Suitability depends on the grade, manufacturing controls, specification, documentation, and applicable regulatory requirements.
What is monobasic potassium phosphate?
Monobasic potassium phosphate is potassium dihydrogen phosphate, commonly represented as KH₂PO₄.
What does a Monobasic potassium phosphate manufacturer provide?
A Monobasic potassium phosphate manufacturer supplies the material according to defined purity, assay, packaging, and quality specifications.
Why is grade selection important?
Different grades may have different purity, impurity limits, test methods, documentation, and intended uses.
Can monobasic potassium phosphate be used in buffering systems?
It can be used in phosphate-based buffering applications where appropriate to the formulation requirements.
Why is batch traceability important?
Traceability links a supplied batch to its manufacturing, testing, packaging, and quality records.
What is a Certificate of Analysis?
It is a batch-specific document reporting analytical results against the established product specification.
What should be included in a quotation request?
Buyers should provide the product, grade, quantity, specification, packaging, destination, intended application, and required documentation.
Media Contact
Pharmaceutical Ingredient Enquiries
Phone: +86 29 8569 1802
Email: sales@xawanlong.com
Official Website: https://www.xawanlong.net/